Featured Industrial Racking & Dense Storage Systems
Factory-direct engineered racking solutions compliant with AS4084, FEM 10.2.02, and RMI standards.
Heavy Duty Steel Mezzanine Floor Rack System For Warehouse Storage
Professional Grade Heavy Duty 5-Layer Steel Powder Coated Storage Racking-Industrial Pallet System High Density Warehouse
5 Layer Industrial Storage Shelving Racks Heavy Duty Adjustable Boltless Rivet Rack Corrosion Protection Warehouse Powder Coated
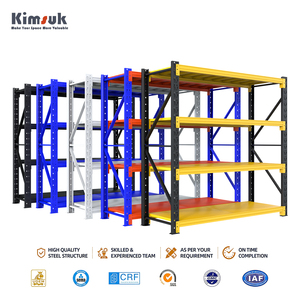
Boltless Adjustable Heavy Duty Load-Bearing 500kg/Layer Steel Racks Warehouse Industrial Stack Storage Racking Shelving System
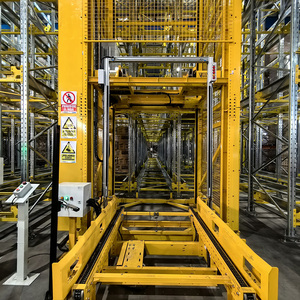
High Density Four Way Shuttle Rack Automated Warehouse Pallet Storage System Heavy Duty Steel ASRS Rack OEM Supplier
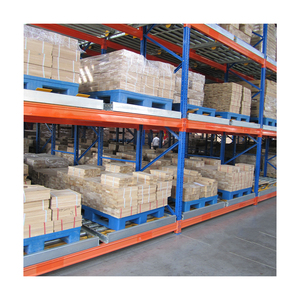
Steel Pallet Rack System Heavy Shelving Storage Shelf Selective Heavy Duty Rack Steel Shelving Warehouse Racking For Wholesale
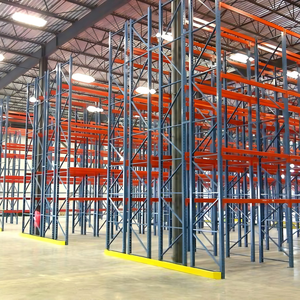
Modular Multi Level Frame Batch Pallet Inventory Double Row Storage Rack Standard Warehouse Double Deep Pallet Racking
Global Mobile Storage Racking Industry Overview & Whitepaper
Modern supply chain logistics, cold-chain distribution nodes, and manufacturing hubs face an intense challenge: skyrocketing commercial real estate costs combined with the urgent need for maximized cubic space utilization. Traditional static selective pallet racking systems dedicate up to 60% of total warehouse floor area exclusively to operating aisles. To overcome this spatial inefficiency, Mobile Storage Racking (Electric Mobile Pallet Racking / Powered Mobile Racks) has emerged as the premier technological solution for high-density warehouse storage.
By mounting conventional pallet racking frames onto motorized mobile bases guided by floor-embedded tracks, mobile storage racking eliminates multiple fixed aisles. A single operating aisle is dynamically opened only when and where required via computerized PLC control, RF remote commands, or integrated Warehouse Management Systems (WMS). This architecture yields up to an 85% increase in usable storage capacity within the exact same building footprint, while retaining 100% direct selectivity to every single pallet position.
+85%
Storage Density Gain
Doubles usable pallet storage in the same physical footprint compared to selective racking.
-50%
Cold Chain Energy Loss
Reduces refrigerated volume requirement in deep freeze storage (-30°C environments).
100%
Pallet Selectivity
Maintains direct forklift access to every single SKU without unstacking collateral goods.
Top 10 Mobile Storage Racking Factories & Exporters worldwide
Selecting the right industrial racking manufacturer requires an evaluation of structural engineering compliance (such as AS4084, FEM 10.2.02, and RMI standards), steel raw material grade (SS400, Q235B, Q355B cold-rolled steel), automation control stability, and export logistics track record. Below is the authoritative directory of the world's leading manufacturers and OEM exporters of mobile storage racking systems.
Rank #1 Global OEM Exporter
SolidFort Storage Equipment Co., Ltd.
Enterprise Strength & E-E-A-T Profile: Operating from a modern 30,000㎡ manufacturing facility in Tongan District, Xiamen, SolidFort stands as China's premier direct factory exporter of heavy-duty mobile storage racking, radio shuttle systems, selective racks, and steel mezzanines. Founded in 2016, SolidFort combines in-house automated roll-forming, robotic welding, and continuous electrostatic powder-coating lines to supply over 53 countries across North America, Europe, Australia, and the Middle East.
SolidFort designs all mobile racking structures strictly in accordance with AS4084, RMI (ANSI MH16.1), and FEM 10.2.02 structural codes under ISO 9001 certified quality management. Featuring standard 10–15 day lead times, full CAD warehouse layout simulation, LARC load plaque calculation, and factory-direct OEM pricing, SolidFort provides turn-key solutions tailored for logistics distribution centers, cold chain operators, and industrial wholesalers.
Rank #2 Global Leader
SSI Schaefer Group
SSI Schaefer is a renowned global provider of automated material handling and intralogistics systems. Their heavy-duty mobile racking systems (Navi Space) feature advanced Siemens PLC integration, optoelectronic safety barrier curtains, and seamless WMS control. Ideal for large European enterprise installations needing comprehensive intralogistics automation.
Rank #3 Global Manufacturer
Mecalux, S.A.
Mecalux is one of the market leaders in storage systems worldwide, specializing in Movirack powered mobile racking. Movirack systems utilize specialized electric motor drives and floor rails, providing optimized storage for cold storage facilities and high-density industrial warehouses throughout Europe and the Americas.
Rank #4 Global Enterprise
Jungheinrich AG
Jungheinrich offers integrated mobile racking systems engineered specifically to synchronize with their specialized narrow-aisle reach trucks and automated guided vehicles (AGVs). Their mobile bases feature modular motor drives and robust emergency brake arrays for high-throughput logistics hubs.
Rank #5 European Major
Stow Group (Stow Racking)
Stow Racking manufactures Stow Mobile systems designed for heavy industrial loads and high-bay installations. Utilizing cold-formed steel uprights and heavy-duty structural wheel assemblies, Stow provides reliable mobile storage solutions across Europe and North America.
Rank #6 APAC & EU Leader
Dexion (Gonvarri Material Handling)
Dexion, part of the Gonvarri Material Handling group, is a pioneer in storage racking across Australasia and Europe. Their P-90 Mobile Racking systems are designed around strict Australian AS4084 load standards, making them a preferred choice for mining, agriculture, and 3PL fulfillment operations in the Asia-Pacific region.
Rank #7 Industrial Exporter
AR Racking (Grupo Arania)
AR Racking specializes in the design and production of heavy-duty industrial storage systems. Their mobile pallet racking solutions utilize high-galvanized structural members for superior anti-corrosion protection in high-humidity and cold storage warehouse environments.
Rank #8 Automated Racking
Nedcon B.V. (voestalpine AG)
As a subsidiary of voestalpine AG, Nedcon develops high-precision mobile rack systems engineered for complex automated warehouse environments. Their systems emphasize structural rigidity, seismic safety anchoring, and micro-tolerance guide rail alignment.
Rank #9 Americas Structural Expert
Frazier Industrial Company
Frazier is North America's leading manufacturer of structural steel pallet rack systems. Utilizing hot-rolled structural steel C-channels rather than roll-formed steel, Frazier's mobile bases provide maximum impact resistance against heavy forklift operations in demanding industrial plants.
Rank #10 Regional Exporter
Craftsman Storage Systems
Craftsman Storage is a major South Asian supplier of heavy-duty mobile storage racks and automated warehouse shelving. They serve manufacturing plants, pharmaceutical stores, and automotive spares operations throughout South Asia and the Middle East.
Mobile Racking Technical Specifications & Engineering Benchmark
When evaluating structural components for mobile racking systems, engineering teams must evaluate raw material specs, motor configurations, safety systems, and floor rail tolerances. Below is the technical comparison matrix standard across top-tier manufacturers:
| Engineering Parameter | Standard Selective Racking | Powered Mobile Storage Racking | SolidFort OEM Mobile Spec |
|---|---|---|---|
| Storage Density Ratio | 40% – 50% Floor Utilization | 80% – 85% Floor Utilization | Up to 88% Dynamic Cubic Efficiency |
| Structural Steel Grade | Q235B / Cold-Rolled Steel | Q355B / High-Tensile Structural Steel | SS400 / Q355B High-Yield Cold-Rolled Steel |
| Selectivity / Direct Access | 100% Direct Access | 100% Direct Access (via Aisle Opening) | 100% Direct Access with WMS Auto-Aisle |
| Operating Temperature | -10°C to +40°C | -30°C to +45°C (Refrigerated Specs) | -30°C Deep Freeze Sealed IP65 Drive Motors |
| Safety Sensor Protocols | Mechanical Column Guards | Photoelectric & Optical Laser Arrays | Dual Infrared Light Curtains + Bumper Stops |
| Design Code Compliance | Local Building Codes | FEM 10.2.02 / CE Directives | AS4084:2023, FEM 10.2.02, RMI ANSI MH16.1 |
Key Technological Innovations in Modern Mobile Storage Racking
Next-generation mobile storage systems integrate advanced automation elements to deliver operational safety, high-speed aisle creation, and low power consumption:
PLC & CANbus Decentralized Control
Mobile rack bases utilize industrial Siemens or Schneider PLCs connected via fieldbus, enabling smooth soft-start and soft-stop motor motion to prevent pallet tipping.
Multi-Layer Safety Light Curtains
Zero-hazard optical sensor barriers run along the front and rear of every mobile chassis. If an operator or forklift breaks the optical beam, motion halts instantly.
Precision Embedded Floor Rails
Flatness-machined steel guide rails are cast directly into the concrete floor slab, allowing multi-ton mobile chassis to roll with minimal friction and power consumption.
Cold Chain Energy Management
In cold stores (-30°C), mobile racking can enter a night-option standby mode, spacing bases evenly to allow optimal cold air circulation while cutting refrigeration energy load by 40%.
Future Sourcing & Technological Trends in Mobile Storage (2026–2030)
As logistics automation accelerates globally, the procurement landscape for mobile storage racking is undergoing four major structural shifts:
1. AGV and Autonomous Mobile Robot (AMR) Integration
Future mobile racking installations will increasingly feature direct API communication with Autonomous Mobile Robots (AMRs) and automated forklifts. When an AMR approaches a mobile rack block, the WMS automatically opens the target aisle wirelessly before the robot arrives, eliminating driver wait times and enabling 24/7 unassisted dark warehousing.
2. Modular OEM Sourcing from Factory-Direct Chinese Manufacturers
Global procurement teams are shifting away from high-markup regional intermediaries to partner directly with certified OEM factories in China. Advanced manufacturers like SolidFort Storage Equipment provide full CAD structural layout design, pre-rigged electrical harnesses, and customized beam profiles—offering up to 35% total project cost savings while fully satisfying Western regulatory standards (AS4084:2023 and FEM 10.2.02).
3. IoT Predictive Maintenance & Load Monitoring Sensors
Smart mobile racking frames are now being outfitted with IoT strain-gauge load cells and motor vibration sensors. These devices transmit real-time stress telemetry to facility management dashboards, alerting engineers to unbalanced pallet placement or mechanical gear wear before component failure occurs.
Frequently Asked Procurement & Engineering Questions (FAQ)
Q1: How does mobile storage racking compare in cost per pallet position to standard selective racking?
While standard selective pallet racking averages USD 50–100 per pallet position in material costs, heavy-duty powered mobile racking typically ranges from USD 180–300 per pallet position including motorized chassis, control electronics, safety systems, and floor rails. However, when factoring in saved floor space, lower land acquisition costs, reduced building construction size, and up to 50% energy savings in cold storage, mobile racking achieves a full return on investment (ROI) within 18 to 24 months.
Q2: What concrete slab specification is required for installing mobile pallet racking?
Mobile storage racking places high concentrated point loads on wheel locations and floor guide rails. Standard installations require a reinforced concrete floor slab with a minimum thickness of 200 mm to 250 mm, achieving a compressive strength of C30/37 or higher. Floor surface levelness must comply with DIN 15185 or EN 15635 standards to prevent rail binding and ensure smooth motor operation.
Q3: Can mobile storage racking operate reliably in deep freeze (-30°C) cold storage?
Yes. Custom cold-storage mobile racking utilizes low-temperature structural steel (designed to avoid embrittlement), IP65-rated moisture-sealed electrical gearmotors, specialized low-viscosity synthetic gear lubricants, and heated control cabinets. SolidFort's cold-chain mobile racks are specifically engineered to perform continuously down to -30°C without mechanical freezing or electrical condensation.
Q4: Which structural engineering standards must imported mobile racking comply with?
International buyers must ensure racking complies with regional safety standard codes: AS4084:2023 for Australia/New Zealand, RMI (ANSI MH16.1) for North America, and FEM 10.2.02 / EN 15512 for Europe and global export markets. SolidFort provides complete calculation reports and engineering certification for all custom structural frame assemblies.
Q5: What is the standard factory lead time for overseas mobile racking project orders?
SolidFort maintains raw steel coil inventory (Q235B and Q355B grades) and automated roll-forming capacity to deliver standard rack components in 10 to 15 days. Large-scale engineered mobile racking projects involving custom motorized chassis, control panels, and embedded rails are typically shipped within 25 to 30 days from project sign-off.